Modern gear and threaded-component manufacturing is no longer just about removing material or forming a profile. Manufacturers need processes that deliver accuracy, repeatability, surface quality, and dependable production rates—all while keeping costs under control.
Two technologies that play important roles in achieving these goals are skiving gear cutting and thread rolling. Although they serve different manufacturing purposes, both rely heavily on properly engineered tooling. The performance of the cutting or forming tool can directly influence the quality of the finished component.
For manufacturers looking to improve production efficiency, understanding how these processes work—and how to select the right tooling—is a valuable starting point.
Why Tooling Matters More Than It Seems
A production tool does much more than shape a component.
Its geometry determines how material is removed or displaced. Its accuracy affects the final profile. Its material and surface treatment influence wear resistance and tool life. Even small deviations can become noticeable when a component is produced repeatedly in high volumes.
This is especially important for gears and threaded components, where dimensional accuracy and consistency are critical.
For U.S. manufacturers working with demanding production schedules, the goal is not simply to find a tool that works. It is to find tooling that remains stable and predictable throughout the production cycle.
That is where processes such as skiving and thread rolling become particularly interesting.
What Is Skiving Gear Cutting?
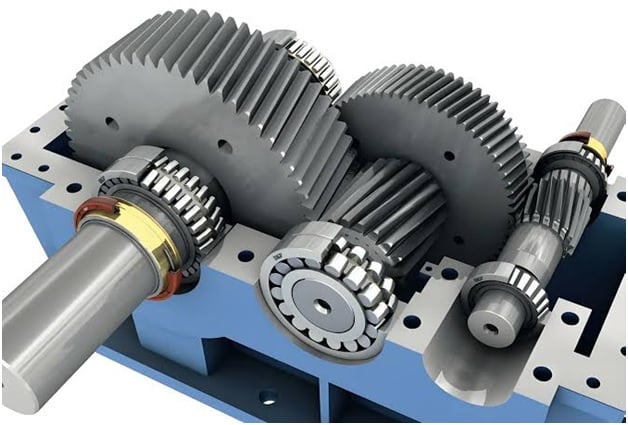
Skiving gear cutting is a gear-manufacturing process that uses a specialized cutting tool to generate gear teeth through a coordinated cutting motion between the tool and workpiece.
Unlike conventional gear cutting methods, skiving combines rotational and axial movements to create a highly productive cutting action. The process is particularly useful when manufacturers need an efficient method for producing internal or external gears.
One of the major advantages of skiving is its potential for high productivity.
The cutting action allows material to be removed efficiently, making the process suitable for applications where production speed and gear accuracy both matter.
However, skiving is not simply a matter of installing a cutter and starting the machine.
Tool geometry, machine setup, workpiece characteristics, cutting conditions, and tool quality all contribute to the final result.
Why Are Manufacturers Turning to Skiving?
Gear production requirements continue to evolve.
Manufacturers often need smaller components, more complex gear geometries, tighter tolerances, and shorter production cycles. Traditional processes may not always provide the most efficient solution for every application.
Skiving can offer several practical advantages, including:
- Efficient material removal
- Potentially shorter machining cycles
- Suitability for internal gear production
- Good production flexibility
- Reduced dependence on multiple manufacturing operations
- Compatibility with modern CNC gear-production equipment
The actual benefits depend on the application and machine configuration, but the process can be particularly attractive for manufacturers seeking a productive alternative for certain gear geometries.
The Tool Is at the Center of the Process
In skiving, cutter design is critical.
The tool must have the appropriate geometry to generate the required gear profile while maintaining the necessary cutting action. Poorly selected or improperly manufactured tooling can lead to profile inaccuracies, excessive wear, vibration, or inconsistent results.
Tool selection should therefore consider factors such as:
Workpiece Material
Different materials behave differently during machining. Harder materials can increase cutting forces and accelerate tool wear, while softer materials may create different chip-formation challenges.
Gear Geometry
The module, pressure angle, tooth count, helix characteristics, and other design factors influence cutter requirements.
Machine Capability
The machine must be capable of providing the required synchronization and movement between the tool and workpiece.
Production Volume
A tooling solution for occasional production may be very different from one intended for continuous, high-volume manufacturing.
Getting these factors right can make the difference between a process that looks efficient on paper and one that performs reliably on the shop floor.
Where Do Thread Rolling Dies Fit In?
While skiving is a cutting process, thread rolling is fundamentally different.
Instead of cutting away material to create a thread, thread rolling forms the thread by displacing material.
This distinction is important.
During rolling, a workpiece is pressed against specially shaped dies. The pressure causes the material to flow into the desired thread form.
The result can be a strong, accurately formed thread with excellent surface characteristics.
For applications where thread strength, consistency, and production speed matter, rolling can be an attractive alternative to conventional thread cutting.
Why Thread Rolling Is Popular in High-Volume Production
Imagine producing thousands—or even millions—of threaded components.
Every second in the production cycle matters.
Thread rolling can provide fast cycle times because the thread is formed rather than individually machined. At the same time, the cold-forming action can contribute to favorable mechanical properties in the finished thread.
Some commonly recognized benefits include:
- High production rates
- Consistent thread geometry
- Reduced material waste
- Good surface finish
- Potential improvements in thread strength
- Efficient repeat production
Of course, successful thread rolling depends on having the correct die design and suitable workpiece material.
That makes choosing experienced thread rolling dies manufacturers in India an important consideration for companies sourcing specialized tooling.
What Should You Look for in Thread Rolling Dies?
Not all rolling applications are identical.
Thread size, pitch, material, blank diameter, production volume, and machine configuration can all affect die requirements.
When evaluating tooling, manufacturers should consider:
Die geometry:
The die must match the required thread specification and forming process.
Dimensional consistency:
Small deviations in die geometry can be reflected across a large production batch.
Material and hardness:
The die must withstand repeated forming forces without premature wear.
Surface finish:
A well-finished die can contribute to smoother forming and consistent component quality.
Application knowledge:
A tooling manufacturer should understand the relationship between die design, workpiece characteristics, and the rolling process.
The right die is therefore not simply a component with a thread profile. It is part of an entire forming system.
Skiving and Thread Rolling Solve Different Problems
It is important not to think of these technologies as competing processes.
They address different manufacturing requirements.
Skiving gear cutting is primarily concerned with generating gear teeth through a controlled cutting process.
Thread rolling, on the other hand, creates external or internal thread forms by plastically deforming the workpiece.
Both processes, however, have something in common: tooling precision directly influences production performance.
In both cases, manufacturers benefit from tooling that is designed around the actual application rather than treated as a generic off-the-shelf component.
Tool Life Should Be Part of the Calculation
A lower initial tooling price does not necessarily mean a lower manufacturing cost.
Consider a production environment where a tool requires frequent replacement. Each replacement can involve:
- Machine downtime
- Tool setup
- Inspection
- Production adjustments
- Scrap risk
- Additional labor
That is why tool life should be considered alongside purchase price.
For high-volume manufacturers, a tool that provides stable performance over a longer production run may deliver significantly better overall value.
Monitoring wear can also help manufacturers determine when tooling should be replaced rather than waiting until component quality begins to decline.
Why This Matters to U.S. Manufacturers
U.S. manufacturers operate in an environment where productivity and consistency are closely connected to competitiveness.
Whether producing automotive components, industrial equipment, power-transmission parts, or precision mechanical assemblies, manufacturers need processes that can maintain quality without unnecessarily increasing production costs.
This makes modern gear-cutting and forming technologies increasingly relevant.
Skiving can help address demanding gear-production requirements, while thread rolling can provide an efficient approach to high-volume threaded components.
The common factor is precision tooling.
A Better Tooling Decision Starts With Better Questions
Before selecting a cutter or die, manufacturers should establish the complete production requirement.
Ask:
- What material will be machined or formed?
- What are the required tolerances?
- What gear or thread geometry is required?
- What machine will be used?
- What is the expected production volume?
- What tool life is required?
- Is the process intended for prototyping, small batches, or continuous production?
- What inspection standards will be applied to finished components?
These questions help narrow the tooling solution and reduce the risk of choosing a tool based only on price or availability.
Precision Is Built Into the Process
High-quality gears and threaded components do not happen at the inspection stage.
They are the result of decisions made throughout production—from material selection and machine setup to tooling design, cutting parameters, forming conditions, and inspection.
That is why skiving gear cutting and thread rolling deserve careful attention.
The technology may be different, but the objective is the same: repeatable manufacturing with dependable quality.
For companies evaluating specialized gear and thread tooling, working with an experienced supplier can help turn that objective into a practical production strategy.
Build the Right Tooling Strategy With SS Tools
The right tooling can influence far more than the shape of a finished component. It can affect cycle time, consistency, tool life, and the overall efficiency of a manufacturing operation.
SS Tools can be considered as a tooling partner when evaluating requirements for gear and thread manufacturing applications. Discussing the application, component specifications, machine setup, and production goals is a practical first step toward identifying the right tooling approach.
When precision matters, the smartest place to start is with the tool that creates it.